2026 Best Heavy Steel Fabrication Suppliers Worldwide

Selecting the 2026 Best Heavy Steel Fabrication Suppliers Worldwide requires more than comparing production capacity or polished websites. This guide examines how suppliers convert engineering drawings into reliable structures, from cutting and forming to welding, coating, inspection, and delivery. A capable fabricator should show qualified welding procedures, traceable material certificates, dimensional control records, and verifiable project experience. The details matter. A misplaced weld, incomplete inspection, or weak corrosion system can create expensive problems long after installation.

As steel-bridge researcher John W. Fisher put it, “Fatigue is a problem of details.” That principle remains highly relevant to heavy steel fabrication, especially for bridges, industrial frames, energy facilities, shipyard components, and large commercial structures. Our evaluation considers workshop capacity, engineering support, quality systems, non-destructive testing, surface preparation, logistics, safety culture, and communication across borders. It also considers whether a supplier can manage real project pressure, including drawing revisions, tight tolerances, weather exposure, and changing delivery schedules.

No worldwide ranking is flawless. Regional standards, transport limits, labor conditions, and project complexity can change the final choice. A supplier with enormous capacity may not suit a smaller, detail-sensitive contract. Another may offer excellent craftsmanship but limited international logistics. This overview therefore presents practical comparisons rather than absolute promises. Buyers should still audit facilities, review recent references, and confirm contractual responsibilities before awarding work. Steel can look simple on a screen. On the workshop floor, every millimeter and weld sequence matters.

2026 Best Heavy Steel Fabrication Suppliers Worldwide

Heavy Steel Fabrication Defined: Plate Above 6 mm and Structural Applications

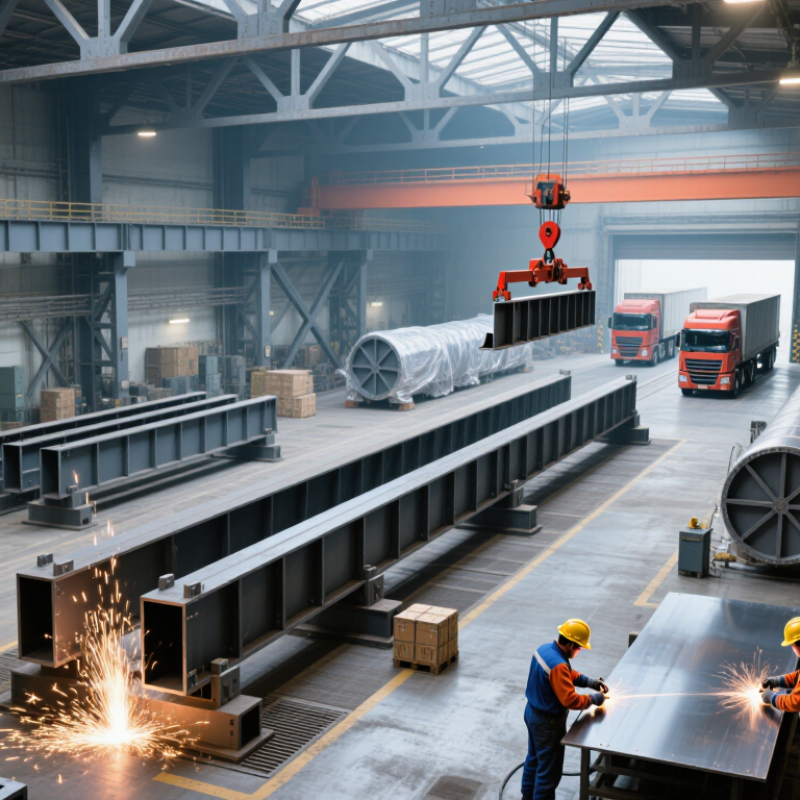
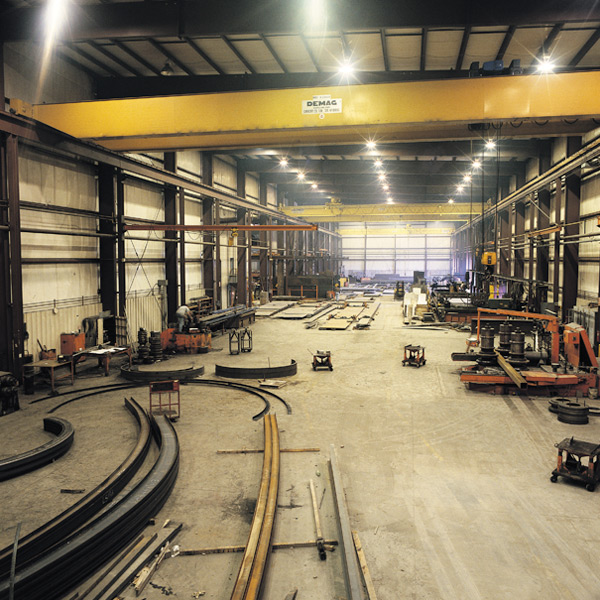
Heavy steel fabrication generally refers to producing components from plate above 6 mm thick. The threshold is practical, not universal. Project specifications may classify thickness differently. In real workshops, plates arrive with mill certificates and heat numbers. Operators cut them using CNC plasma, oxy-fuel, or waterjet systems. The method depends on steel grade and tolerance. Edges often need cleaning before welding. Small preparation errors can create serious fit-up problems.

Structural applications give this category its purpose. Fabricated columns, beams, base plates, trusses, frames, and bridge sections must carry predictable loads. Engineers review drawings, steel grades, weld sizes, and connection details before production. Qualified welding procedures help control distortion, cracking, and incomplete fusion. Inspectors check dimensions, weld profiles, and selected areas using ultrasonic or magnetic-particle testing. Records matter. Traceable records matter more.

For 2026 sourcing, buyers should examine process control rather than factory size alone. Ask for material traceability, welder qualifications, inspection plans, calibration records, and realistic delivery terms. Confirm how suppliers handle oversized parts, tolerances, surface preparation, and protective coatings. Local codes and project standards still govern acceptance. Impressive machinery cannot replace weak documentation. The six-millimeter rule is useful, but it is not enough. Transport limits and lifting points are easy to overlook. That planning gap can delay an otherwise sound steel structure.

Global Supplier Landscape in 2026: Capacity, Regions, and Core Fabrication Services

The 2026 heavy steel fabrication market is defined by regional capacity, delivery discipline, and technical depth. World Steel Association data recorded about 1.88 billion tonnes of crude steel production in 2024. Asia remained dominant, while Europe and North America retained advanced engineering and certification capabilities.

East Asian suppliers often provide large plate processing, tower sections, pressure structures, and modular assemblies. Indian and Middle Eastern fabricators are expanding in energy, infrastructure, and industrial projects. North American workshops remain competitive in engineered components, repair work, and short regional supply chains. European facilities typically emphasize automation, traceability, low-emission production, and complex welded structures. Geography still matters.

Capacity alone proves little. It can mislead. A reliable supplier should show plate thickness ranges, welding procedures, heat-treatment control, machining envelopes, and non-destructive testing records. Coating systems, dimensional inspection, lifting plans, and export packing also deserve review. The OECD Steel Market Developments reports continue to highlight global capacity pressure and uneven demand, which may increase price competition but also create schedule risks.

Buyers should compare verified monthly output, not advertised annual capacity. Ask for recent inspection dossiers and realistic production photographs. Data from the International Energy Agency also shows that steelmaking must reduce emissions sharply this decade. Therefore, energy sources, scrap usage, process efficiency, and emissions reporting are becoming procurement factors. No supplier is perfect. Even strong workshops may struggle with labor shortages, port delays, or incomplete digital records. Supplier selection in 2026 requires evidence, site-level experience, and careful questioning.

Quality Benchmarks: ISO 3834, AWS D1.1, and EN 1090 Execution Classes

2026 Best Heavy Steel Fabrication Suppliers Worldwide

Choosing a heavy steel fabrication supplier in 2026 requires more than comparing tonnage and quoted prices. Quality begins with a controlled welding system. ISO 3834 shows whether the fabricator manages welding personnel, procedures, materials, equipment, and records consistently. Ask to review welding procedure specifications, welder qualifications, material certificates, and inspection plans. A clean workshop helps, but documented control matters more. Certificates alone prove little.

For structural steelwork, AWS D1.1 provides practical requirements for welding design, qualification, fabrication, and inspection. Reliable suppliers should explain how they control preheating, interpass temperature, weld size, and visual inspection. Non-destructive testing should match the project risk, not merely the lowest quotation. Ask for evidence. Records matter. A supplier may satisfy an audit and still produce uneven fit-up on a demanding frame.

EN 1090 execution classes add another useful comparison. EXC1 suits simpler, lower-risk work, while EXC2, EXC3, and EXC4 require progressively stronger controls and documentation. The correct class depends on structural use, consequence of failure, materials, and design requirements. Experienced fabricators connect the class to traceability, dimensional checks, welding coordination, and final inspection. I would not accept vague claims about “international quality.” Site visits and sample reports often reveal more than polished presentations. Even experienced buyers can overlook small issues, such as incomplete heat-number tracking or poorly protected weld areas. That deserves reflection.

2026 Best Heavy Steel Fabrication Suppliers Worldwide - Quality Benchmarks: ISO 3834, AWS D1.1, and EN 1090 Execution Classes

Anonymous supplier benchmarking framework for heavy steel fabrication procurement. Values shown are practical screening benchmarks, not claims of certification or performance by any specific company.

Evaluation Dimension International Reference Baseline Requirement Strong Supplier Benchmark Objective Evidence to Request Procurement Verification Question
Welding quality management ISO 3834-2, ISO 3834-3 or ISO 3834-4 A documented welding quality system appropriate to the complexity and safety relevance of the fabricated structure. ISO 3834-2 for comprehensive quality requirements, supported by controlled welding procedures, inspection plans and traceable records. Valid certificate scope, certification body, expiry date, covered processes, material groups and product types. Does the certificate cover the actual welding processes, materials, thicknesses and production location proposed for the project?
Welding coordination ISO 14731 and ISO 3834 Named personnel responsible for welding coordination and technical control. Qualified welding coordination personnel with clearly defined authority, availability and documented competence. Appointment letter, competence records, welding coordinator qualifications and responsibility matrix. Who has final authority over WPS approval, welder qualification, nonconformance disposition and repair approval?
Structural steel welding AWS D1.1/D1.1M Welding procedures and welder performance qualifications conforming to the contractually specified AWS requirements. Current WPS/PQR or prequalified WPS documentation, qualified welders, controlled essential variables and inspection records. Applicable AWS D1.1/D1.1M edition, WPS register, qualification reports, welder continuity logs and inspector credentials. Are the proposed WPS documents valid for the steel grade, thickness range, welding position, joint type and process required?
European structural execution EN 1090-1 and EN 1090-2 Execution controls appropriate to the required Execution Class and market regulations. Factory Production Control certification under EN 1090-1, welding quality controls aligned with EN ISO 3834, and documented execution procedures under EN 1090-2. FPC certificate, notified-body details where applicable, execution-class scope and manufacturer’s documented production controls. Can the supplier provide documentation for the exact Execution Class, component type and delivery market?
Execution Class capability EN 1090-2: EXC1 to EXC4 Capability matched to the project consequence class and design specification. Demonstrated EXC3 capability for demanding structural work; EXC4 capability only where formally established and project-relevant. Certificate scope, completed-project references without confidential client data, inspection plans and independent audit findings. What documented experience and certified scope support the proposed EXC level?
Material traceability EN 10204; project specification Heat-number traceability from incoming steel through cutting, fabrication and final release. Full digital or controlled-paper traceability linking mill certificates, part identification, weld maps, inspection results and shipment records. Sample material certificates, traceability matrix, transfer-of-marking procedure and identification photographs. Can every critical fabricated part be traced back to its original heat number after cutting and assembly?
Non-destructive testing ISO 17635; ISO 9712; project specification NDT methods and examination percentages defined by weld category, design requirements and applicable standard. Qualified Level 2 personnel, independent Level 3 technical oversight where required, calibrated equipment and controlled reporting. NDT personnel certificates, written practices, calibration records, weld maps and sample reports. Are NDT percentages based on the governing design code and risk category rather than a fixed percentage applied to every weld?
Dimensional control EN 1090-2; project drawings and tolerances Inspection of overall dimensions, hole locations, straightness, squareness, fit-up and assembly interfaces. Inspection and Test Plans with hold points, calibrated measurement equipment and documented as-built dimensional reports. Calibration certificates, inspection templates, 3D measurement records and final dimensional reports. How are dimensional deviations assessed, approved and corrected before coating or shipment?
Heavy fabrication capacity Project-specific technical schedule Capacity must be demonstrated against the actual maximum part size, mass, plate thickness and lifting requirements. Documented production envelope, adequate cranes, welding bays, turning equipment, blasting and painting facilities, and controlled subcontracting. Equipment list, crane inspection records, bay dimensions, maximum lifting capacity and production-flow plan. What are the verified maximum lifting weight, component length, plate thickness and assembly envelope at the proposed facility?
Cutting and edge preparation EN 1090-2; ISO 9013; project specification Cutting, bevel geometry, heat-affected areas and edge quality controlled according to the applicable specification. CNC cutting with controlled nesting, documented bevel checks, repair procedures and traceable post-cut identification. Cutting plans, edge inspection records, machine calibration or maintenance records and sample inspection reports. How does the supplier control heat input, bevel accuracy and material identification after thermal cutting?
Surface preparation and coating ISO 8501-1; ISO 8502; ISO 8503; ISO 12944 Specified preparation grade, surface profile, environmental conditions and coating thickness controls. Controlled blast-cleaning and painting environment with soluble-salt checks, dew-point monitoring, DFT measurements and repair records. Coating procedure, paint technical data sheets, environmental logs, surface-profile readings and dry-film-thickness reports. Which corrosion category, durability period, preparation grade and coating system are included in the quotation?
Quality inspection independence ISO 9001; project Inspection and Test Plan Inspection responsibilities are defined and inspection results are retained. Quality personnel can stop work or reject nonconforming output without production-pressure conflicts. Organization chart, ITP, inspection release procedure, NCR log and corrective-action records. Can the quality function independently issue a hold point, reject a weld or require a repair without production approval?
Subcontractor control ISO 9001; ISO 3834; contract requirements Critical outsourced operations are identified and controlled. Approved-subcontractor register, flow-down requirements, audit records and verification of certificates before work starts. Subcontractor evaluation forms, purchase-order quality clauses and outsourced-process inspection records. Which operations are subcontracted, and how are welding, NDT, coating and traceability requirements flowed down?
Delivery and logistics Incoterms® 2020; project logistics plan Packaging, lifting points, transport route, customs documentation and delivery sequence are defined. A load-out plan integrating component identification, center of gravity, lifting studies, sea or road transport constraints and site sequencing. Transport method statement, packing list, lifting plan, photographs and delivery-risk register. How will oversized components be protected, lifted, identified and delivered in the required installation sequence?
Documentation and handover Project quality plan; ISO 3834; EN 1090; AWS D1.1/D1.1M Final dossier includes certificates, inspection records, NCR disposition and release documentation. Indexed manufacturing record book with complete traceability, signed inspection releases, approved deviations and digital searchability. Redacted sample dossier, document register, transmittal procedure and retention policy. Can the supplier provide a sample final manufacturing dossier showing traceability from material receipt to shipment?
Commercial transparency Contract and technical specification Quotation clearly separates fabrication, testing, coating, engineering, packaging, transport and optional work. Transparent assumptions, exclusions, inspection allowances, escalation conditions, lead times and change-control mechanism. Redacted quotation template, responsibility matrix, schedule baseline and change-order procedure. Which quality, inspection, engineering and logistics activities are excluded from the stated fabrication price?
Supplier selection score Buyer-defined weighted evaluation Pass/fail screening for mandatory certificates, technical capability, financial capacity and delivery feasibility. Recommended weighting: quality compliance 30%, technical capability 25%, delivery 20%, traceability and documentation 15%, commercial value 10%. Completed technical questionnaire, certificate verification, factory audit and reference-project evidence. Are mandatory compliance items treated as pass/fail before commercial scoring is applied?
Important scope note: ISO 3834 certification, AWS D1.1/D1.1M compliance and EN 1090 Execution Class capability are not interchangeable. The applicable requirement depends on the governing design code, project location, structural consequence, contract specification and intended use. Certificate scope, issuing body, validity and production location should be independently verified before award.

Supplier Evaluation Metrics: Tonnage, Welding Accuracy, Lead Time, and Traceability

2026 Best Heavy Steel Fabrication Suppliers Worldwide

Choosing a heavy steel fabricator requires more than checking equipment lists or annual revenue. Tonnage shows capacity, but it does not prove consistent execution. Ask whether the supplier can handle your required plate thickness, assembly weight, lifting plan, and monthly output. A 5,000-ton capacity claim means little without recent production records. Inspect completed structures, not only polished brochures.

Welding accuracy should be measured through qualified procedures, trained welders, dimensional reports, and non-destructive testing records. Review weld maps and inspect critical joints before shipment. Small alignment errors can become expensive during installation. Laser measurement helps, but human judgment still matters. Tolerances must match the project specification, not a convenient internal standard.

Lead time should include engineering review, material purchasing, cutting, welding, coating, inspection, and delivery. Request a milestone schedule with realistic buffer time. Traceability connects every plate to its heat number, mill certificate, weld, inspection result, and revision history. Digital records are useful when they remain complete and readable. A perfect dashboard cannot repair missing documents. Supplier audits, sample files, and direct discussions with production staff often reveal more than sales presentations. Some evaluations remain uncertain, and that uncertainty deserves a documented risk allowance.

2026 Best Heavy Steel Fabrication Suppliers Worldwide

Supplier Evaluation Metrics: Tonnage, Welding Accuracy, Lead Time, and Traceability

The chart presents anonymized industry benchmark tiers rather than company-specific results. Capacity is shown as annual fabricated steel tonnage, welding accuracy represents the percentage of welds accepted without repair, lead time is the typical production window in weeks, and traceability indicates the percentage of material and welding records maintained through final delivery. Higher scores indicate stronger performance; lead time is reverse-scored because shorter delivery periods are preferred. The evaluation framework is aligned with common practices under ISO 3834, ISO 5817, EN 1090, and EN 10204.

Comparing Leading Suppliers by Certifications, Industries, and Project Scale

The 2026 heavy steel fabrication market favors suppliers with verified skills, not impressive brochures. Compare certifications such as ISO 9001, ISO 3834, EN 1090, and qualified welding procedures. These standards indicate controlled processes, traceability, and inspection discipline. However, certification alone proves little. A supplier may hold valid documents but lack recent experience with complex structures.

Industry experience should match your project’s risks. Bridge components require fatigue control and precise dimensional checks. Energy facilities demand strict welding records and non-destructive testing.

Industrial platforms need durable coatings, safe access designs, and reliable site coordination. Ask for anonymized case studies, inspection reports, and evidence of similar load requirements.

Project scale matters too. A workshop producing small frames may struggle with a 5,000-ton assembly. Large capacity can also create communication gaps. I have seen both problems.

Tips:

Request a production schedule, material certificates, weld maps, and final inspection procedures before signing. Confirm plate thickness limits, crane capacity, machining accuracy, and packing methods. Visit the facility when practical. A video tour is useful, but it cannot reveal every weakness. Compare suppliers by delivered performance, not quoted weight alone. Lead time, rework history, engineering support, and export coordination often determine the real cost. Leave room for uncertainty. Steel prices, port delays, and design changes can quickly reshape a project plan.

Request a Quote